
PET Preform Moulds · 9 min read
Published: October 16, 2026
PET Preform Mould Parting Line and Flash Control: A Buyer Validation Guide
Set a practical, traceable acceptance boundary for PET preform parting lines and flash before mould shipment.
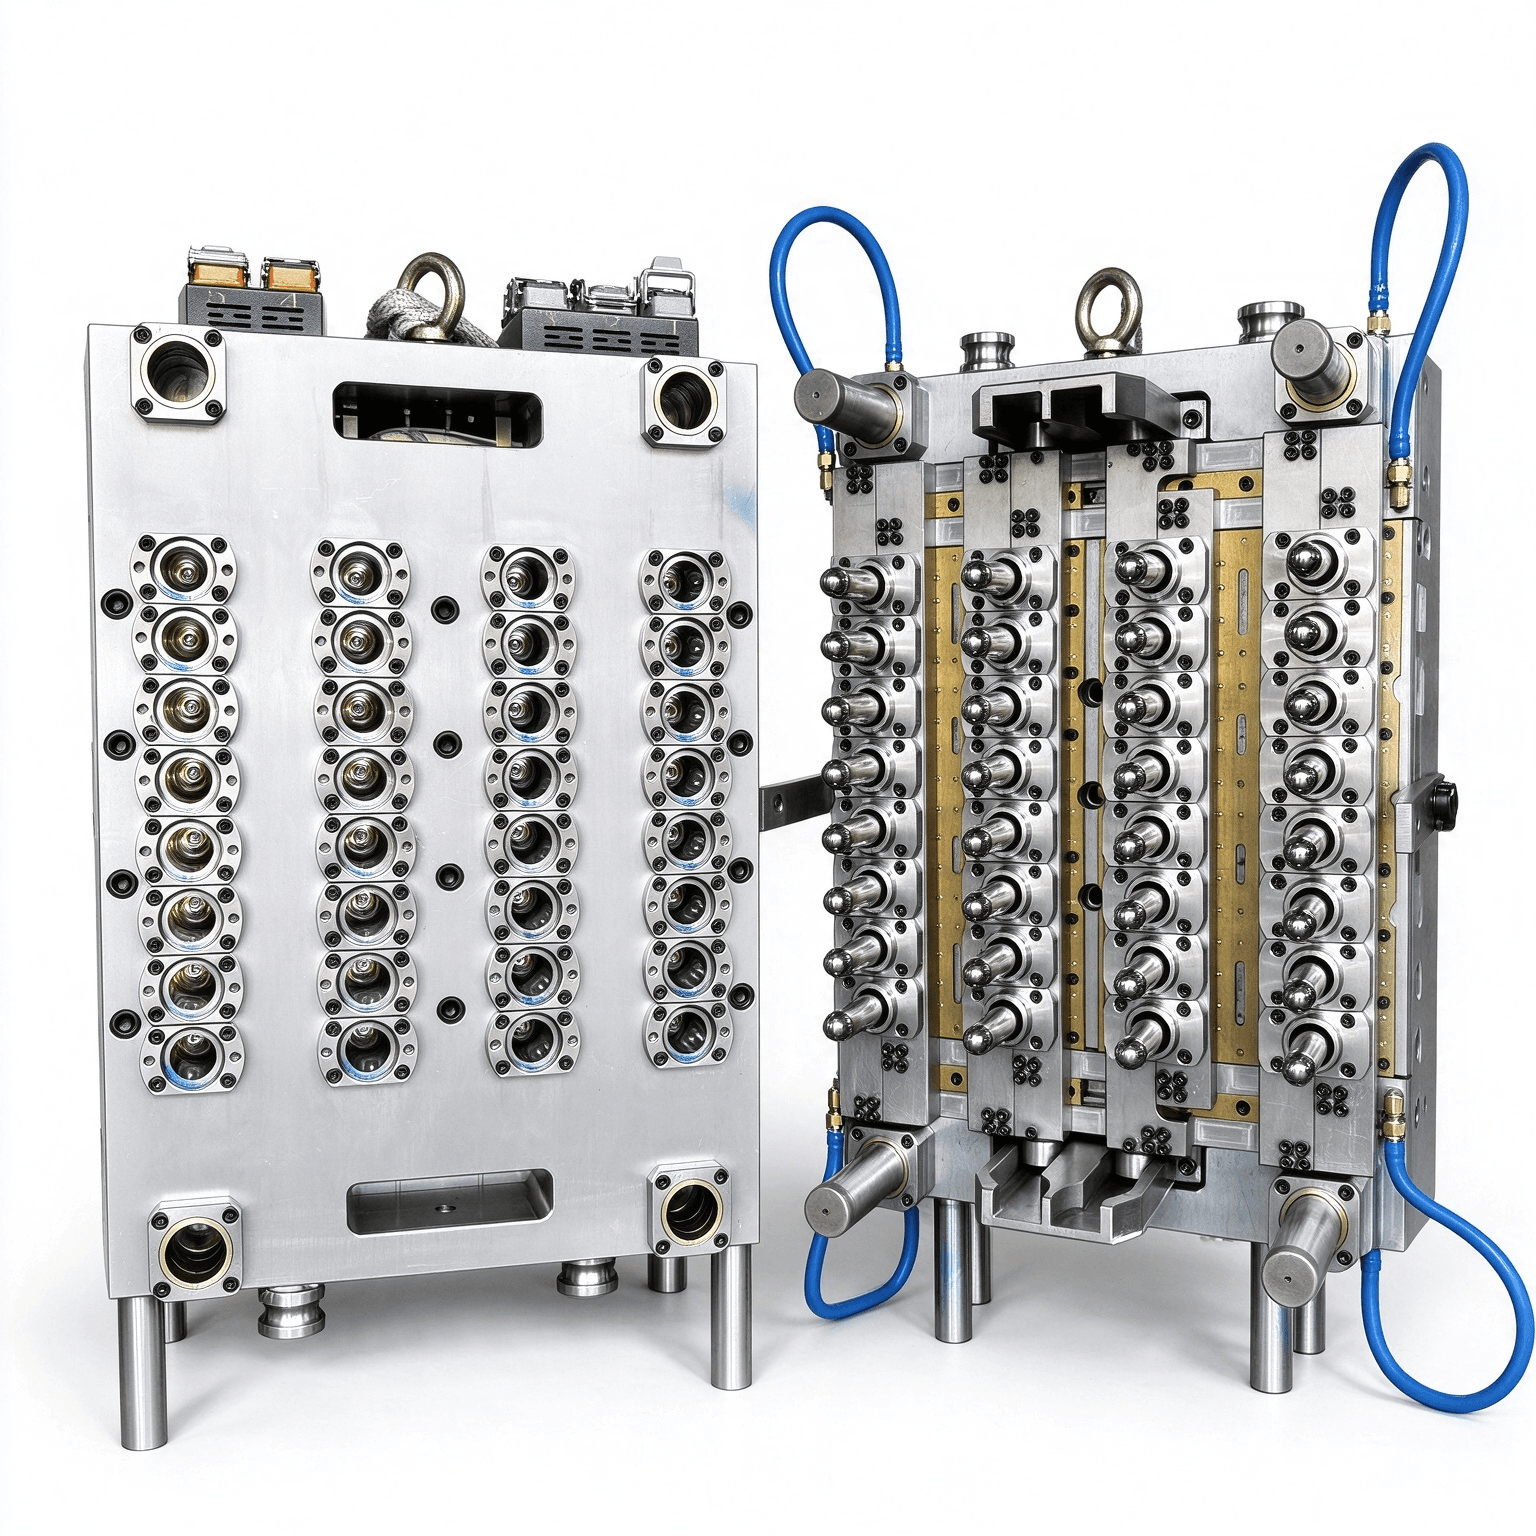
Flash at a PET preform parting line can create handling, visual and downstream blow-moulding problems. A useful buyer specification does not simply say “no flash”: it defines the drawing boundary, sampling condition, inspection method and response when one cavity differs from the rest.
Define the acceptance boundary before the trial
Use the approved preform drawing to identify the neck, support ring, body and gate zones where a parting line is functional or cosmetic. Agree how samples will be conditioned, illuminated and measured. This prevents a supplier and buyer from judging different conditions after the mould is built.
| Control point | Define before FAT | Evidence to keep |
|---|---|---|
| Drawing | Revision, critical zones and permissible witness line | Approved drawing |
| Samples | Cavities, quantity and conditioning time | Cavity-labelled sample set |
| Process | Resin, dryer, temperatures, pressure and cycle | Stable-trial record |
| Inspection | Visual method, magnification and dimensional check | Inspection sheet and photos |
| Actions | Owner and retest condition for any exception | Open-action log |
Sample every cavity under a stable condition
Separate a cavity pattern from a process change
Record the cavity number on the selected samples and keep the process condition fixed while collecting them. A line appearing in one cavity may point to local alignment, insert wear or vent condition; a pattern across all cavities may instead relate to clamp force, material, packing or temperature. Do not change several inputs before preserving the evidence.
Inspect the complete functional zone
Check the neck finish, thread, support ring, body and gate transition. A visually small flash can still affect a cap interface, transfer system or blow-mould handling. Where the drawing calls for a dimension near the parting line, document the instrument and result rather than relying on a general appearance statement.
Turn exceptions into a controlled corrective action
The supplier should identify the suspected cause, adjustment made and cavity samples used for the retest. The buyer should confirm whether an observed witness line is within the agreed cosmetic boundary or whether it affects function. Retain before-and-after evidence with the final FAT report so the receiving factory starts from a known mould condition.
Frequently asked questions
Is every parting line a defect?
No. A controlled witness line may be normal. The acceptance decision depends on the approved drawing, application and any functional impact.
Why must samples be identified by cavity?
Cavity identification shows whether the issue is local or repeats across the tool, which makes corrective action traceable.
Can higher clamp force always remove flash?
No. Flash can involve fit, wear, pressure, temperature, material condition or venting. Raising clamp force without diagnosis can hide the cause.
Should flash be checked only at the mould supplier?
No. The FAT establishes a baseline. The receiving factory should preserve that report and compare early commissioning samples under its own documented conditions.
What belongs in the handover package?
Include drawings, cavity map, stable-trial settings, sample and inspection records, photos, corrective actions and the final retest result.
Talk to a mould engineer
Request a parting-line review: Send your approved preform drawing, PET grade, cavity target, quality boundary and injection-machine details for a practical validation plan.
Get a Quote →