
Plastic Bucket Moulds · 12 min read
Published: September 27, 2026
Plastic Bucket Mould RFQ and Factory Acceptance Checklist for Packaging Buyers
A bucket mould is part of a complete packaging system. Use this buyer guide to define product interfaces, production inputs, factory acceptance evidence and shipment preparation before release.
SEO information
- **SEO title:** Plastic Bucket Mould RFQ & Factory Acceptance Checklist for Buyers
- **Meta description:** Specify and source a plastic bucket mould with confidence. Use this RFQ and acceptance checklist for pails, lids, handles, IML, cooling, trials, shipment and installation.
- **URL slug:** `plastic-bucket-mould-rfq-factory-acceptance-checklist`
- **Primary keyword:** plastic bucket mould
- **Secondary keywords:** plastic pail mould, bucket mould RFQ, IML bucket mould, bucket mould factory acceptance test, plastic bucket mould supplier
- **Search intent:** Transactional / procurement risk reduction
For paint pails, food containers, chemical packaging, household storage and agricultural products, a bucket mould is part of a larger packaging system. The finished pail must stack, carry, seal, label and survive its intended handling conditions. The mould therefore needs to be evaluated beyond its external appearance: part geometry, resin, lid and handle interfaces, cooling, ejection, automation, trial evidence, maintenance access and export handover all influence the real cost of production.
This guide gives purchasing teams a practical framework for requesting and accepting a plastic bucket mould. It is written for projects that may use round, rectangular or oval buckets, lids, handles and in-mould labels. Exact dimensions and acceptance limits should always come from the approved product drawing and application—not from a generic mould catalogue.
Define the bucket before you define the mould
The most useful mould RFQ begins with the finished package. Send the product drawing or samples and identify the intended application. A food tub, paint pail and chemical bucket can have similar shapes but different requirements for resin, wall distribution, sealing, drop resistance, stacking and labelling.
Include the following data:
- bucket volume, top diameter or length/width, bottom dimensions and height;
- target part weight, wall-thickness expectations and permitted cosmetic areas;
- resin grade, melt-flow behaviour and any approved recycled-content plan;
- lid drawing, gasket or sealing concept, tamper evidence and matching samples;
- handle type, handle material, handle-lug geometry and assembly sequence;
- IML artwork dimensions, label material, label location and robot/static-control details if IML is required;
- product filling condition, expected contents, transport and stacking requirement;
- required annual output, number of shifts, injection-machine data and target production window;
- inspection requirements: dimensional report, lid fit, handle fit, leak, top-load, stack, drop or other application tests.
This is not paperwork for its own sake. It helps the mould engineer identify sensitive areas before design release: the rim that must seal to the lid, the handle lug that sees repeated stress, a thin wall that affects filling, or a label area that needs consistent surface and robot clearance.
Bucket, lid and handle are one system
Many late-stage tooling problems happen because the bucket was designed separately from the lid and handle. A mould can produce a visually good bucket that still has a poor lid snap, inconsistent rim diameter or handle interference. Share all mating components before the mould design is frozen.
Lid and rim fit
The bucket rim is often a critical functional feature. Its geometry affects the sealing or snap condition with the lid, opening force, tamper-evident behaviour and stackability. Agree which rim dimensions are critical, how they will be measured and whether a customer-supplied lid is available for the factory trial.
Handle lugs and assembly
Handle lugs need adequate strength, geometry and clearance. Their moulding and ejection should be reviewed with the actual handle style. If the handle is fitted after moulding, document whether the customer or supplier will prove assembly during the trial. The goal is not to add unnecessary tests; it is to avoid discovering a basic interface issue after the mould has travelled overseas.
Choose mould design around the production cell
Cavity count and machine fit
Bucket moulds are commonly single-cavity or multi-cavity depending on bucket size, annual volume, machine capacity and automation. Start with required good buckets per hour, then check the entire cell: projected area and clamp-force basis, shot size, plastication recovery, mould height, tie-bar spacing, opening stroke, ejector arrangement, take-out, cooling and available floor space.
Do not ask a supplier to select a cavity count from volume alone. A 20-litre pail and a small food tub are very different tools even if both are called “buckets.” The supplier should explain the assumptions behind the recommendation and identify any missing machine data.
Gate, runner and cooling choices
Gate position, runner concept and cooling layout influence weight control, cycle time, weld-line location, cosmetic appearance and deformation. For high-volume programmes, a hot-runner arrangement may reduce runner waste and help stabilise filling, but it adds equipment, controls and maintenance considerations. A simpler runner can suit a lower-volume programme if the buyer accepts its material and handling implications.
Cooling deserves the same attention as steel selection. The bucket base, rim, sidewall and handle-lug areas do not cool in the same way. Inadequate or unbalanced cooling can lead to long cycles, ovality, warpage or an inconsistent lid fit. During design review, ask for a clear cooling-circuit concept, utility assumptions and connector layout. During installation preparation, confirm water quality, flow, filtration, temperature control and access for leak checks.
Steel and wear parts
The appropriate steel and surface treatment depend on expected volume, resin, corrosion exposure, polish requirement, maintenance capability and the design of the critical areas. Do not select a steel grade based on a marketing slogan. Instead, ask the supplier to identify which steels are proposed for the mould base, cavity, core, inserts and slides, and explain why. Where the agreed scope includes heat treatment, request the relevant records.
For long-running bucket programmes, access to gate inserts, ejector components, slides and seals matters. A serviceable design with an agreed spare-parts list can reduce downtime more effectively than an unrealistically low maintenance claim.
When IML changes the mould project
In-mould labelling can give a retail bucket a durable branded surface, but it introduces more interfaces. The label must enter the cavity accurately, remain correctly positioned during injection and release with a clean appearance. That requires coordination among mould geometry, label material, static control, vacuum or robot end-of-arm tooling, opening stroke and process conditions.
For an IML bucket RFQ, add label drawings, label material, print tolerance, artwork orientation, expected robot model, label pickup method and allowable position variation. If automation is supplied by a separate company, define the interface: who confirms robot clearance, vacuum ports, timing signals, safety sequence and trial responsibilities? The mould supplier can design for the agreed interface, but cannot validate equipment it never sees.
A buyer-friendly plastic bucket mould RFQ checklist
Use the following structure when requesting quotes:
- **Product:** bucket drawing/revision, volume, dimensions, weight, resin and application.
- **Mating parts:** lid, handle, gasket, tamper feature and physical samples where possible.
- **Appearance:** label/IML requirements, texture, permitted gate location and visible areas.
- **Production:** annual demand, required good output, planned shifts and actual machine data.
- **Tool scope:** cavities, runner/hot runner, controller, automation interfaces, spares and installation support.
- **Quality:** agreed dimensions, sample quantities, functional checks and test responsibilities.
- **Evidence:** trial report, photographs/video, inspection record, final drawings/manuals and packing photos.
- **Commercial process:** drawing approval, design review, trial stages, acceptance milestone, shipment method and warranty/service boundaries.
This RFQ format gives suppliers enough information to produce comparable proposals and helps purchasing teams identify quotation gaps. It is particularly useful when multiple countries, factories or packaging partners are involved.
Factory acceptance test: what to inspect before release
A factory acceptance test (FAT) is the buyer's chance to verify the agreed tool function before the cost and delay of overseas shipment. The exact acceptance plan varies by project, but the following sections are a practical baseline.
1. Confirm identity and documentation
Check mould number, cavity count, drawing revision, nameplate information and the list of included accessories. Verify that the agreed technical documents are being prepared, including water-circuit diagram, electrical or hot-runner information where relevant, spare-parts list and trial record.
2. Inspect mould function before material is introduced
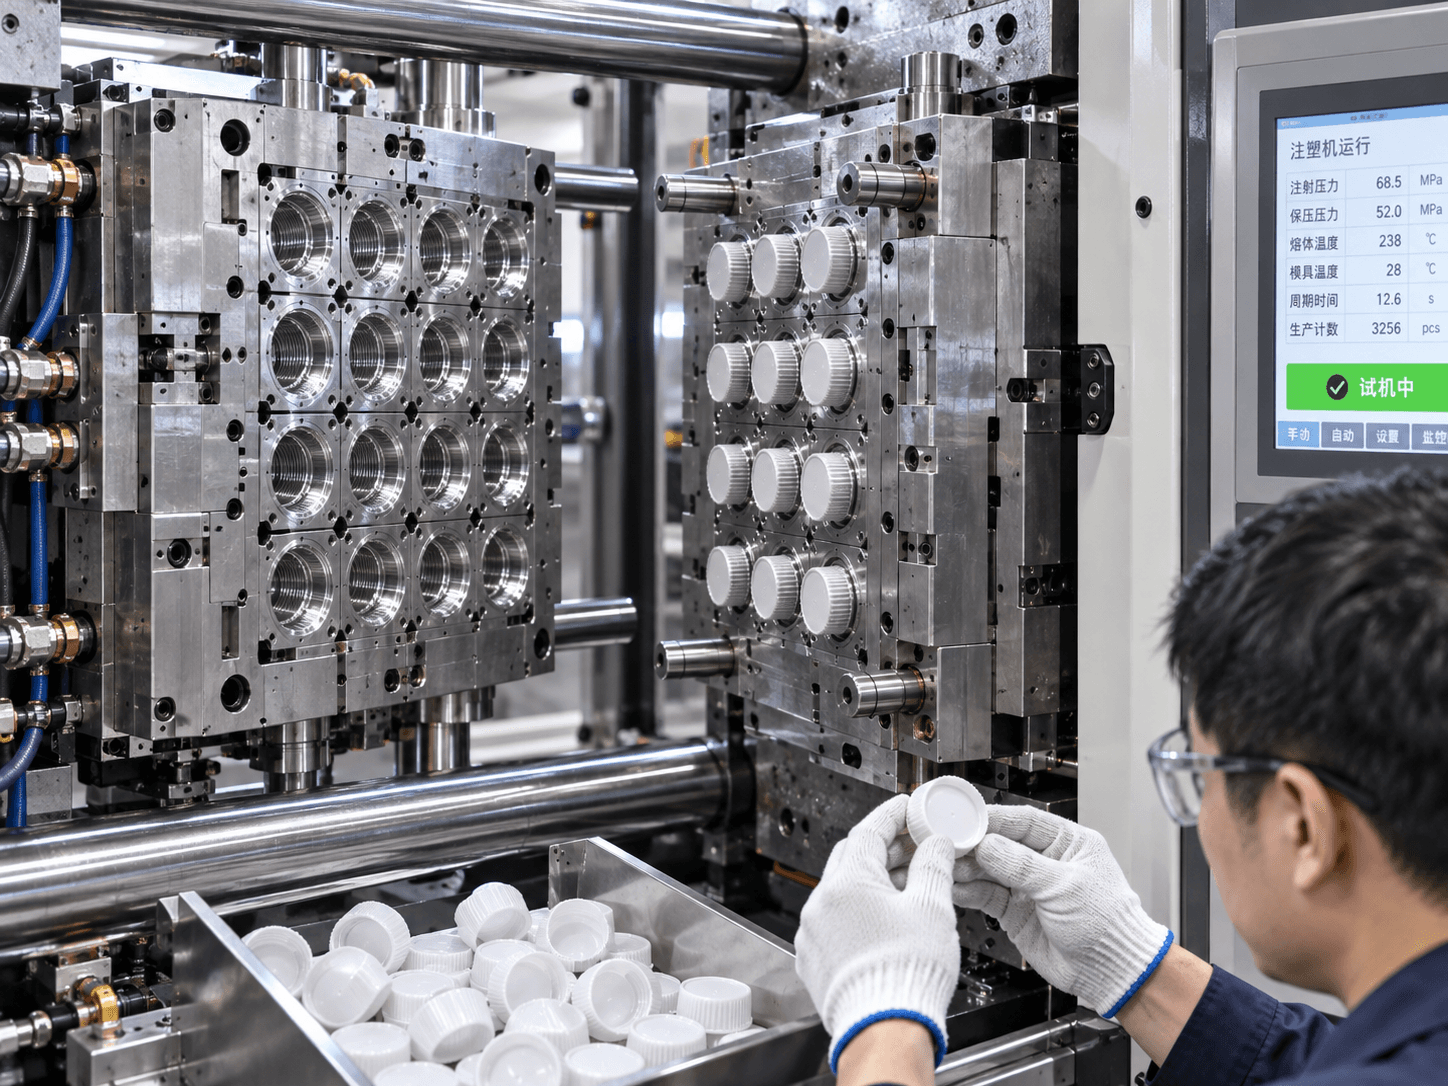
Observe opening, closing, guiding, slides, lifters, ejection and any unscrewing or special mechanism. Movements should be smooth, protected and repeatable. This does not replace production testing, but it can reveal a mechanical issue before the trial time is spent on process adjustments.
3. Check cooling and heating circuits
Confirm circuit labels, connections, flow direction and leakage checks. For hot-runner tools, confirm controller compatibility, zones, sensors, cabling and basic heating response. The goal is to verify the agreed system and prepare the receiving factory for installation—not to claim a universal performance value without the site's actual utilities.
4. Run stable production cycles
Ask for a meaningful continuous trial after conditions have stabilised. Record resin, basic process conditions, mould temperature or cooling context, cycle indication and sample identification. One good shot is useful for an engineering discussion; a stable run is better evidence of repeatable operation.
5. Inspect parts and functional interfaces
Review bucket appearance, fill, gate area, flash, sink, warpage and the drawing dimensions agreed as critical. Test lid and handle fit with the approved mating components. Where the application requires it, plan appropriate leak, stack, top-load or drop testing with a clear method and responsibility. For IML products, check label position, wrinkles, adhesion appearance and repeatability under the agreed production setup.
6. Close corrective actions before shipment
If a problem is found, document the issue, proposed change, owner and re-test. A transparent corrective-action record is more useful than verbal assurance. Release the mould only after the buyer and supplier agree how each relevant item has been closed or transferred into a documented follow-up plan.
Shipment inspection and receiving-factory preparation
Before export packing, inspect the mould and accessories together. Confirm corrosion protection, water removal or preservation approach, protected connectors, lifting-point information, loose-part packing, spare-part identification, internal restraint and crate condition. Ask for photographs before the crate is sealed and for exterior marks showing mould number, dimensions, weight and handling direction.
The receiving factory should prepare machine compatibility, utilities, lifting capacity, temperature controllers, water lines, resin drying/handling, take-out or IML equipment, safety interface and the trial-team schedule before arrival. Keep the supplier's final trial report available during installation; it provides a starting point, not a substitute for local optimisation.
Frequently asked questions
What should I include in a plastic bucket mould RFQ?
Include the bucket drawing, volume, target weight, resin, lid and handle details, label or IML information, annual output, injection-machine data, required tests and preferred scope for runner, controller, spares and shipment records.
Why are lid and handle samples important?
They help validate the bucket's mating interfaces at factory test. Rim fit, handle-lug clearance and assembly issues are faster and less costly to resolve before export than after installation.
Is a hot runner always better for a bucket mould?
Not always. It can reduce runner waste and help some high-volume projects, but it adds controls, maintenance and cost. Evaluate it against bucket size, production volume, resin, cycle target and the operating capability of the receiving factory.
What should be checked during a bucket mould factory acceptance test?
Verify mould identity, mechanisms, cooling/heating systems, stable production, critical dimensions, lid and handle interfaces, agreed application tests, documentation, spares and export packing. The details should be agreed in the purchase scope.
Talk to a mould engineer
Ready to source a pail, bucket, lid or IML mould? Get a Quote by sending your bucket drawing, lid/handle details, resin, annual output and injection-machine data. SHUNYOU can help structure the RFQ, trial scope and shipment handover checklist.
Get a Quote →