
PET Preform Moulds · 11 min read
Published: September 30, 2026
PET Preform Mould Cavity Balance: Factory Acceptance and Sampling Guide
Turn PET preform cavity balance from a vague claim into documented factory-acceptance evidence before shipment.
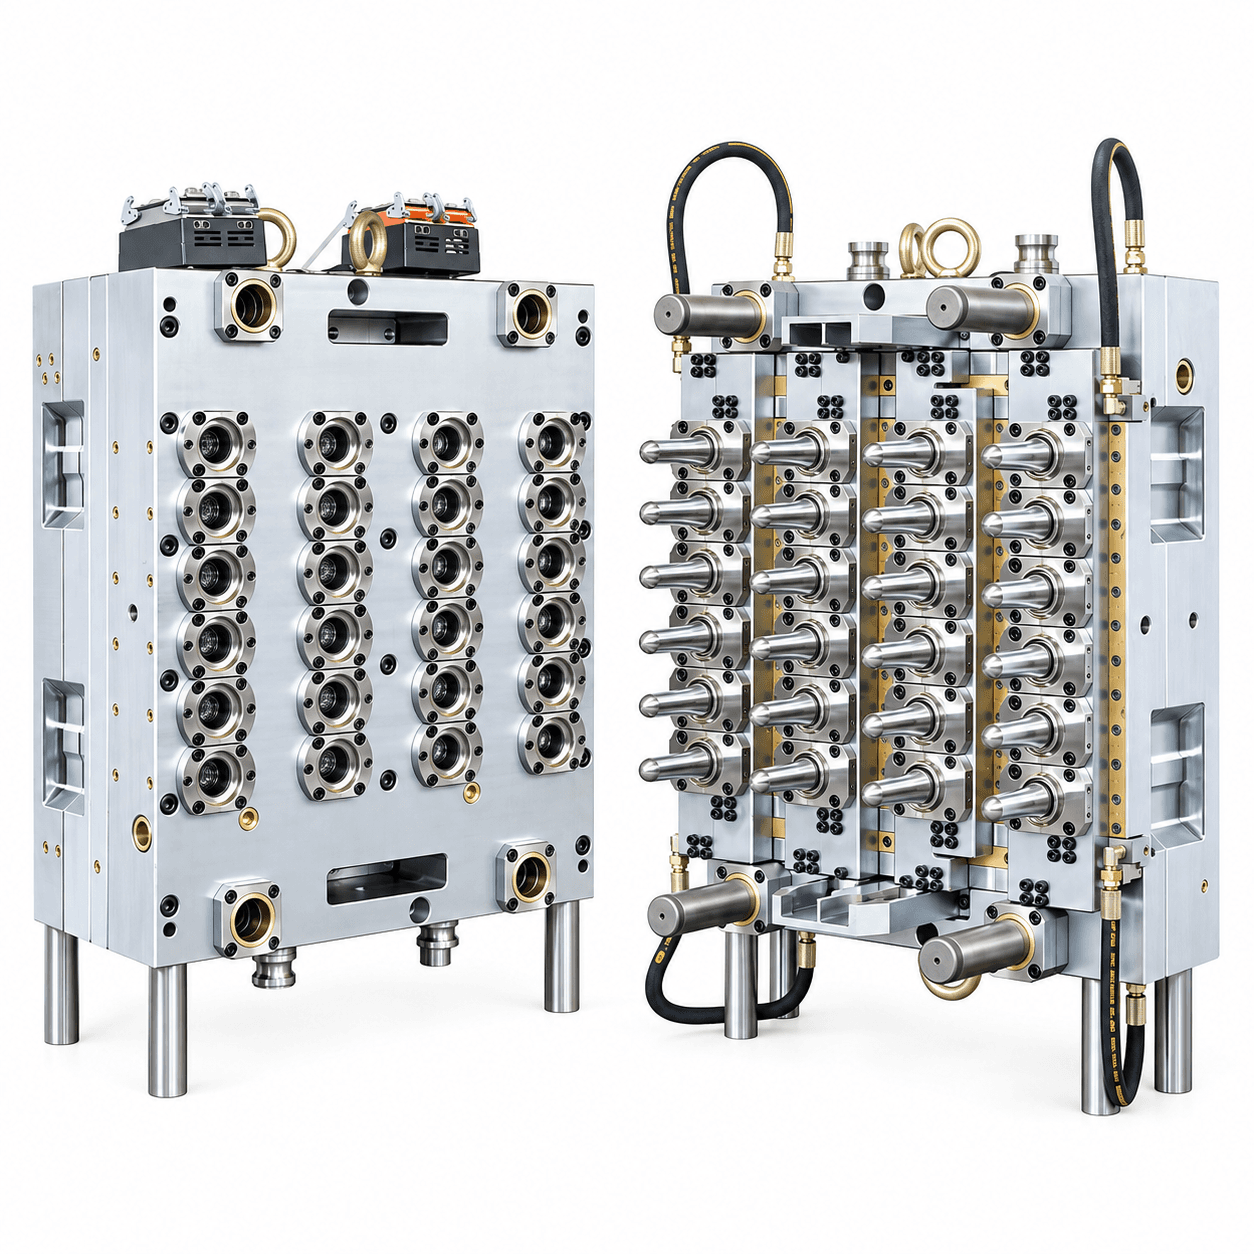
A PET preform mould can open, close and produce visually acceptable parts while still carrying cavity-to-cavity variation that becomes costly during sustained production. For beverage, edible-oil and household-packaging buyers, cavity balance should therefore be a defined factory-acceptance topic, not an informal observation made from a handful of samples.
This guide explains what balance means in a multi-cavity PET preform tool, how to prepare a useful factory acceptance test (FAT), which records to request, and how to avoid treating one trial result as a universal guarantee. It is written for buyers who need evidence before shipment without asking a supplier to promise results that depend on resin, machine and operating conditions.
What “Cavity Balance” Means in a PET Preform Mould
In practical terms, balance describes how consistently cavities fill and produce preforms under one documented process condition. Buyers often see it through part weight, gate appearance, neck dimensions, wall distribution, colour and visual condition. It is not a single property of the hot runner alone.
The injection machine, PET grade, drying condition, regrind policy, melt temperature, injection profile, cooling-water condition, mould alignment, venting and handling can all influence the result. A balanced manifold is important, but it has to work with the complete production cell.
Why it matters after the mould leaves the factory
Small variation can affect downstream blow moulding, bottle weight control, cap fit and line scrap. A preform that looks acceptable near the press can behave differently after reheating and stretch blow moulding. That is why the buyer should identify the product characteristics that actually matter to the finished package rather than relying only on a visual pass/fail statement.
Define Acceptance Before the Trial
The best FAT begins before machining is complete. Put the agreed product revision, resin, neck finish, preform weight, cavity count, injection-machine model and expected inspection items in the purchase specification. If matching bottle or closure checks are required, say so early enough for samples and fixtures to be available.
| Buyer input | Why it belongs in the FAT plan |
|---|---|
| Approved preform drawing and neck-finish data | Establishes the correct product revision and measurement references |
| Resin grade and preparation requirement | Helps make the trial condition traceable rather than generic |
| Cavity identification plan | Lets sample results be linked to individual cavities |
| Sampling quantity and inspection method | Avoids collecting attractive samples only |
| Acceptance priorities | Separates critical dimensions, appearance and useful process observations |
Do not copy a tolerance or balance number from another project unless the same part, resin, test method and production context apply. A credible supplier will explain the method, not simply present an impressive percentage with no conditions attached.
Build a Useful Sampling Plan
Identify every sample
Ask for cavity identification or another agreed traceability method. A sample without an identified cavity cannot help a buyer see whether a condition is local or systemic. Record the process setting, resin batch where practical, date, tool number and sample sequence alongside the inspection sheet.
Sample across the mould, not only from one location
For a multi-cavity tool, collect samples across the manifold layout. The exact quantity should be agreed for the project, but the principle is simple: the sampling plan must make it possible to compare zones and repeat an observation. Where practical, retain representative samples for buyer review or later comparison after installation.
Separate short-shot diagnosis from production samples
Short-shot work can reveal filling behavior; it is not the same as a finished-preform acceptance result. If a diagnostic short-shot study is requested, document its purpose, process condition and conclusions separately from full-part inspections. This avoids incorrectly treating a troubleshooting exercise as a production specification.
What to Record During Factory Testing
Factory testing should show more than a running mould video. Request a concise record containing the condition under which samples were made and the checks actually performed.
- Injection-machine identification and relevant process window
- Resin and material-preparation information supplied for the trial
- Cycle time observed during the agreed stable run, without presenting it as a guaranteed site cycle
- Cooling-water connection and condition information available at the factory
- Sample identification, weight or other agreed measurements, and visual observations
- Gate, neck and ejection observations
- Open points, corrective actions and any limitations of the trial
When a question appears, ask whether the issue correlates with a cavity, a process adjustment, water condition, resin condition or handling. This is more useful than immediately assuming that a cavity insert is defective.
Inspect the Interfaces that Affect Balance
Hot runner and temperature control
Confirm the stated zone count, wiring identification, controller interface, heater and thermocouple documentation, and spare-component references. The purpose is not to prescribe a brand; it is to make service, diagnostics and installation practical.
Cooling and mould movement
Review cooling connection labels, water-path documentation, visible leakage checks, mould opening and closing, ejection and safety features. Cooling stability can influence both cycle behavior and preform consistency, so the receiving plant needs clear connection information rather than a collection of unlabelled hoses.
Handling and post-mould condition
Preforms can be marked or distorted after ejection if transfer and collection are not considered. Record how samples were handled during the trial and distinguish mould-related evidence from marks introduced after mould opening.
Shipment Inspection and Installation Preparation
Before dispatch, verify that the mould is preserved, water and electrical connections are marked, lifting points are identified and the agreed spare parts, drawings, manuals and trial records are packed or supplied digitally. Shipment photos should show the condition before crating and the protection used for exposed surfaces.
At the receiving factory, recreate the FAT discipline: confirm utilities, controller compatibility, water connections, machine interface, safety clearance and sample traceability before declaring the line stable. The first production trial should be treated as site commissioning, not as proof that the factory test was meaningless.
Common Buyer Mistakes
The most common mistake is accepting “samples are good” without defining which samples, under what conditions and against which drawing. Other avoidable mistakes include changing resin or neck design after trial, requesting an unrealistic cycle time without defining utilities, and comparing cavity data collected with different inspection methods.
Balance evidence should reduce uncertainty. It cannot remove normal process responsibility from the moulder after the tool is installed.
Frequently asked questions
Does a balanced factory trial guarantee identical production at our plant?
No. It provides traceable evidence under the documented trial condition. Resin, drying, machine, water, ambient conditions and operating practice at the receiving site can change the result.
Should every cavity be measured during FAT?
Agree the approach in advance. For critical projects, cavity traceability and broad coverage are valuable. The appropriate inspection depth depends on the product, risk and acceptance plan.
Is part weight the only balance check?
No. Weight is useful, but buyers may also need to assess neck dimensions, gate condition, appearance, wall distribution and downstream functional fit.
Talk to a mould engineer
Request a PET preform FAT review: Send your preform drawing, resin, cavity count, machine information and acceptance priorities for a practical sampling and documentation proposal.
Get a Quote →