
PET Preform Moulds · 10 min read
Published: October 15, 2026
PET Preform Mould Wall Distribution and Blow-Moulding Transfer: A Buyer Validation Guide
Connect preform wall distribution with bottle performance through drawing-led checks, stable samples and a documented stretch-blow transfer plan.
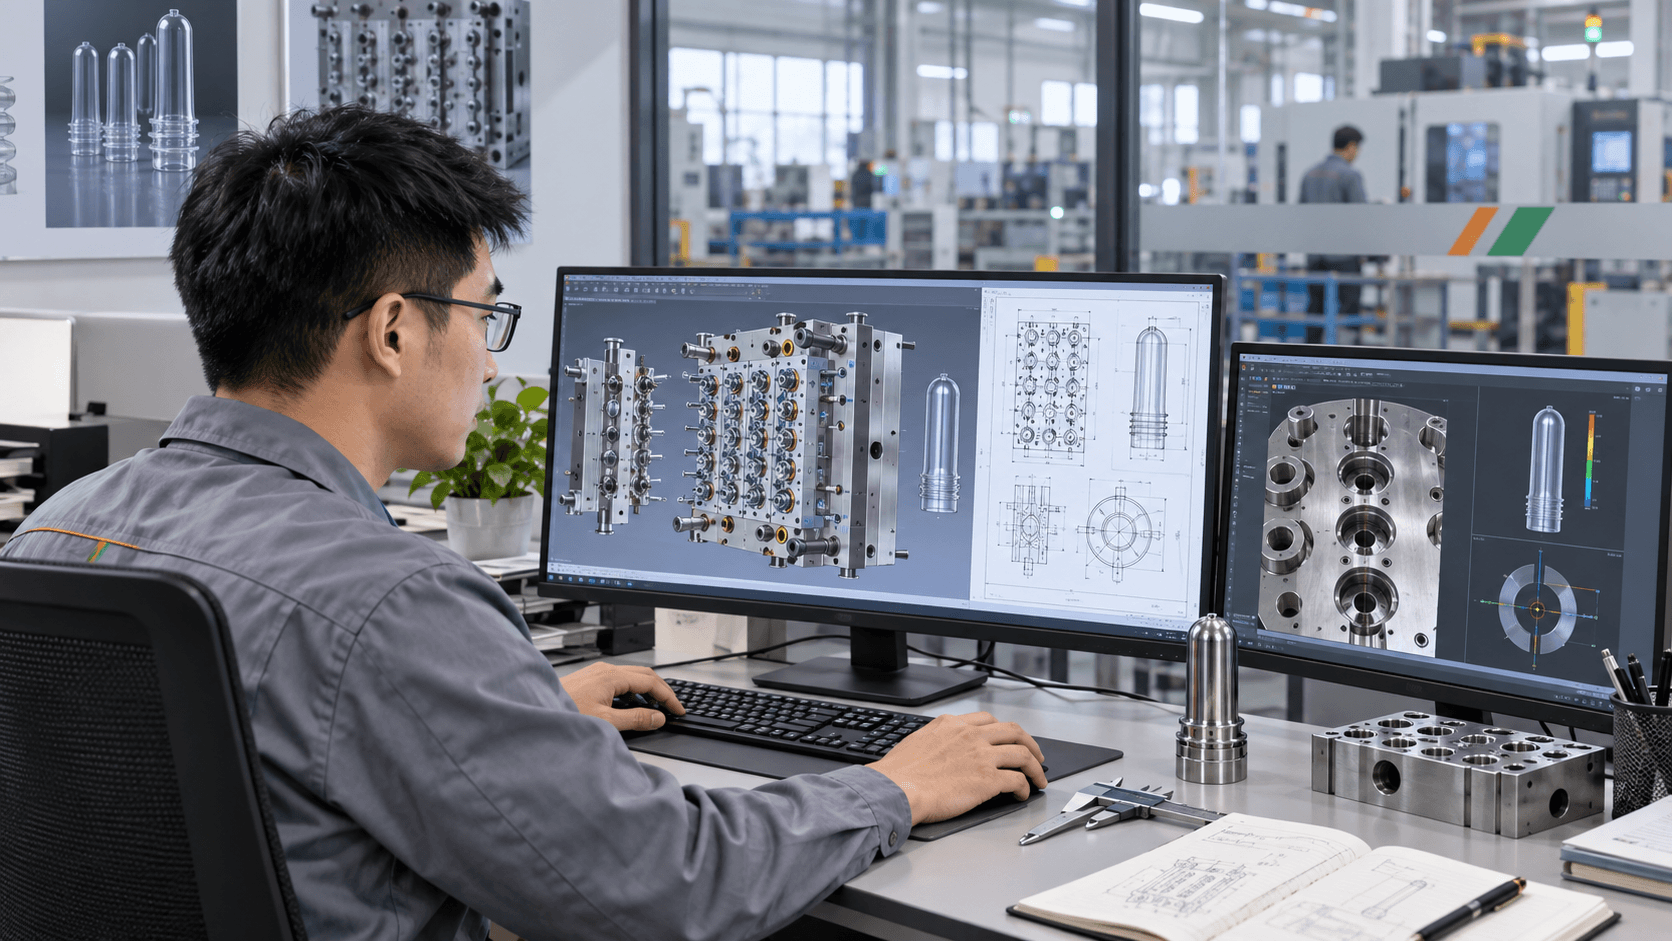
The preform is not the final package. Its wall distribution has to support the approved bottle shape, stretch-blow process and end use without turning a factory trial into an unsupported promise. Buyers should translate bottle requirements into a measurable preform plan, then keep the injection trial and blow-moulding transfer connected by labelled samples and recorded conditions.
Start With the Bottle, Not a Generic Thickness Number
Use the approved bottle drawing, fill volume, neck finish, base geometry, label area and service conditions as the design boundary. A nominal preform weight alone does not describe where material is needed after stretching. Agree the relevant drawing revisions and identify critical bottle zones before mould design release.
| Review point | What to define | Evidence to retain |
|---|---|---|
| Bottle programme | Approved drawing, volume, neck and base | Controlled drawing revision |
| Preform | Weight, length, gate and measurement locations | Preform drawing and sampling plan |
| Material | PET grade, colour or additive boundary | Material identification record |
| Injection trial | Machine, hot runner, cycle and cavities | Stable-trial sheet and cavity map |
| Blow transfer | Stretch-blow machine and approved operating window | Blow trial record and labelled bottles |
Create a Drawing-Led Sampling Plan
Measure locations that explain the result
Define the measurement method, instruments, conditioning and locations before sampling. Include the preform zones that influence the bottle body, shoulder, base and gate transition. A result should be comparable between the mould supplier, converter and brand owner; it should not depend on one operator's visual judgement.
Identify samples by cavity and trial condition
Retain labelled samples from the agreed cavities after the process is stable. Record the mould revision, resin lot, dryer condition, barrel and hot-runner settings, cycle time, cooling and take-out method. This record helps distinguish a cavity pattern from a change in material, machine or process.
Transfer the Check Into Stretch-Blow Moulding
Injection acceptance and bottle qualification are linked but not interchangeable. At the blow stage, record the relevant preform identification, reheating condition, stretch and blow programme, bottle mould revision and inspection result. Compare bottles from the agreed preform samples with the approved bottle criteria, rather than interpreting a favourable result from an unknown sample as mould acceptance.
Agree What FAT Can Prove
The mould supplier can demonstrate preform samples under an agreed injection condition. The receiving factory and its bottle-development team remain responsible for confirming final performance with their actual blow equipment, process and product requirements. Use an open-action list for items that must be confirmed after transfer; this is clearer than making the mould FAT carry claims outside its scope.
Frequently asked questions
Can one preform weight guarantee bottle performance?
No. Weight is one input. Bottle performance also depends on the approved geometry, material, distribution, reheating, stretch-blow conditions and the end-use requirement.
Which preform samples should be sent for blow trials?
Use stable, labelled samples from agreed cavities and record the mould revision, resin lot and trial settings. Avoid mixed samples without a traceable origin.
Is visual inspection enough for wall distribution approval?
No. Visual inspection can support the review, but the project should agree measurement locations, method, tolerances and the bottle checks that matter for the application.
Does a bottle problem always mean the preform mould is wrong?
No. The cause can involve preform design, resin condition, injection process, reheating, stretch-blow settings, bottle moulding or handling. Preserve the records before changing tooling.
What should be included in the handover package?
Include controlled drawings, cavity map, stable-trial sheet, sample identification, measurement results, material record, open actions and the agreed transfer or commissioning plan.
Talk to a mould engineer
Request a wall-distribution review: Send your bottle and preform drawings, PET grade, target weight, stretch-blow machine details and quality priorities for a practical validation plan.
Get a Quote →