
Mould Engineering · 10 min read
Published: September 28, 2026
How to Choose Mould Steel for Plastic Caps, Preforms and Packaging Parts
A steel list is useful only when it connects cavity, core and base materials to the resin, product features, production environment and maintenance requirements. This guide gives buyers the questions to ask before comparing tooling quotations.
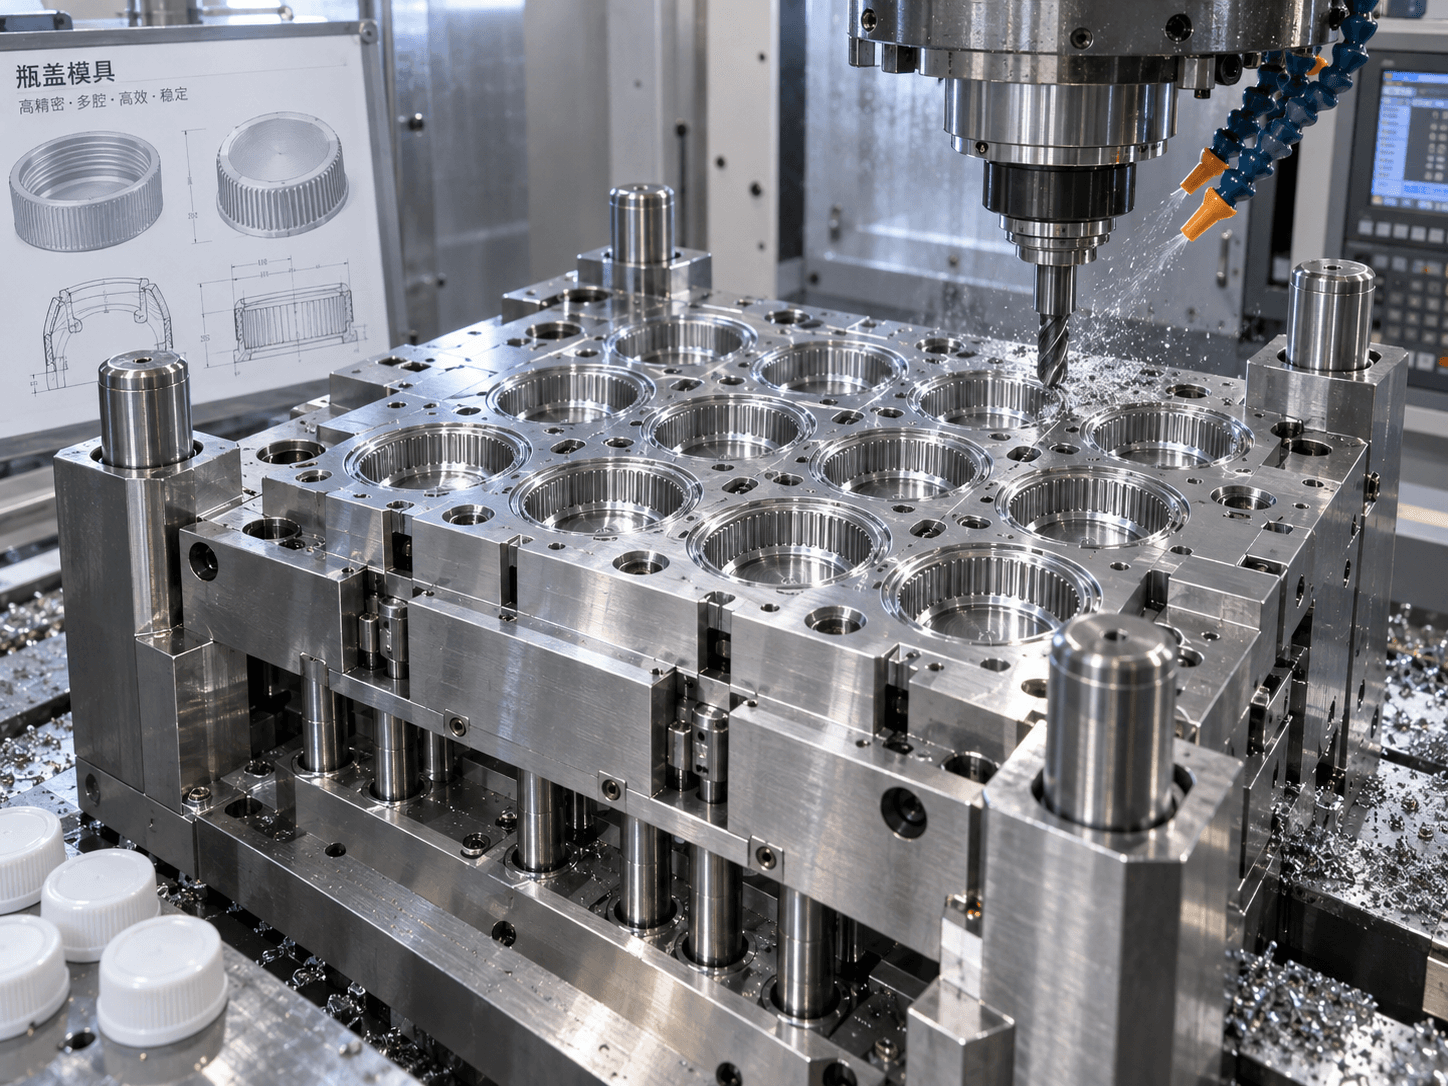
Steel selection is one of the most consequential decisions in an injection mould quotation, but it is often reduced to a short line such as “S136 cavity/core, P20 mould base.” That line is useful only when it is connected to the part, resin, expected production conditions, finish requirement and maintenance plan. A higher-grade material does not automatically solve every moulding issue, and an inexpensive grade is not automatically unsuitable. The goal is to select material properties that match the real risk.
For packaging components, the relevant risks can include corrosion from resin additives or cooling water, wear at threads and sliding interfaces, polishing requirements, repeated opening and closing, colour changes and access for maintenance. A cap, PET preform, bucket or food-container project should therefore define which plates and inserts carry which function before a buyer compares material names.
Separate cavity/core steel from mould-base steel
Cavity and core inserts shape the moulded part. Their selection can be influenced by surface finish, wear, corrosion resistance, heat treatment, repair strategy and the critical features of the product. The mould base provides the structural platform for plates, guide elements, cooling, ejection and any side actions. It is evaluated differently: rigidity, machining practicality, plate thickness, support and the arrangement of moving components matter alongside the base material grade.
This distinction avoids a common procurement mistake: comparing two steel lists without comparing what each list actually covers. A proposal should identify the cavity, core, thread inserts, sliders, wear plates, base plates and any special inserts. If an item is not specified, ask whether it is included in the proposed grade or left to the supplier’s standard practice.
Relate material choice to resin and operating environment
Resin is an engineering input, not just a commercial material name. The resin family, fillers, recycled content, colour masterbatch, processing temperature and cleaning method can affect wear and corrosion risk. In packaging projects, water quality and long-term storage can also affect cooling circuits and exposed surfaces. The expected environment should be discussed before design release.
Stainless or corrosion-resistant grades may be considered where corrosion resistance, polishability or specific product requirements justify them. Pre-hardened grades can be practical for base components and many applications where a controlled, economical specification is appropriate. The correct choice depends on the application. Claims about tool life should be tied to stated operating assumptions, inspection and maintenance, rather than presented as an unconditional promise.
Consider surface finish, functional details and repair access
Some components require a polished sealing surface, fine thread, optical or high-gloss appearance, textured finish or a demanding release condition. Other areas may need toughness around moving mechanisms or a wear-resistant insert at a local high-load feature. One mould can therefore use more than one steel strategy.
Ask the supplier to identify the critical product features and explain how they will be protected. For example, cap threads, tamper-band geometry, sealing land and hinge detail deserve a different discussion from the exterior base plate. The same is true for a PET preform neck finish, gate region and cavity surface. If a component is designed as a replaceable insert, confirm how it will be identified, removed and requalified after service.
Put the steel specification into the RFQ and acceptance plan
An RFQ should state the requested or approved material grades, any acceptable alternatives, heat-treatment expectations where relevant, certificates required, hardness-check method if applicable, and the parts to which each requirement applies. It should also identify any customer standards that must be followed. This creates a meaningful basis for comparing quotations.
At factory testing and shipment inspection, verify the tool identification, cavity count, supplied documentation, spare inserts or components, and the condition of visible functional surfaces. Where material certificates or heat-treatment records are part of the agreed scope, include them in the handover package. A factory trial proves running behaviour under the documented conditions; it does not replace a clear material traceability record.
Avoid over-specifying steel without evidence
It is reasonable to ask for a material upgrade when the resin, output, corrosion exposure or surface-finish requirement supports it. It is less useful to specify the most expensive grade everywhere without considering machining, lead time, repairability and the actual failure mode. A practical technical review asks: what will wear, what may corrode, what must be polished, what needs to move, and how will the receiving factory maintain it?
This approach gives purchasing teams a better way to discuss price differences. Instead of asking only which supplier uses “better steel,” ask which component receives which material, why it is used, what evidence will be supplied and how it supports the intended production environment.
Frequently asked questions
Does S136 automatically mean a mould will last longer?
No. Material choice is one factor. Tool life also depends on design, resin, processing conditions, cooling-water quality, handling, preventive maintenance and the specific components exposed to wear.
Can one mould use different steel grades?
Yes. A mould commonly combines a base material with different grades or inserts for cavities, cores, threads, sliding elements or high-wear areas. The specification should make the allocation clear.
What steel documents should be requested before shipment?
Request the documents agreed in the order: material certificates, heat-treatment records where applicable, mould specification, spare-parts list and any inspection record that identifies the mould and components.
Talk to a mould engineer
Mid-article CTA placement: after “Put the steel specification into the RFQ and acceptance plan.” Use “Send Your Requirements” with: “Share your product drawing, resin and output target for a component-by-component mould steel review.”
Get a Quote →